
A sweet solution: Swisslog automates confectionery handling for Mondelēz, supporting a 60% increase in storage capacity

The customer - a global confectionery manufacturer
Mondelēz is one of the largest snacking companies in the world, with global net revenues of approximately US$38.5 billion (approx. AUD$55.2 billion) in 2024.
Mondelēz holds the number one global position in biscuits (cookies and crackers) and number two in chocolate, while also growing rapidly in baked snacks.

Operational efficiency

Flexibility, storage capacity and scalability

Proven performance

Significant savings
The challenge - consolidating a complex distribution network
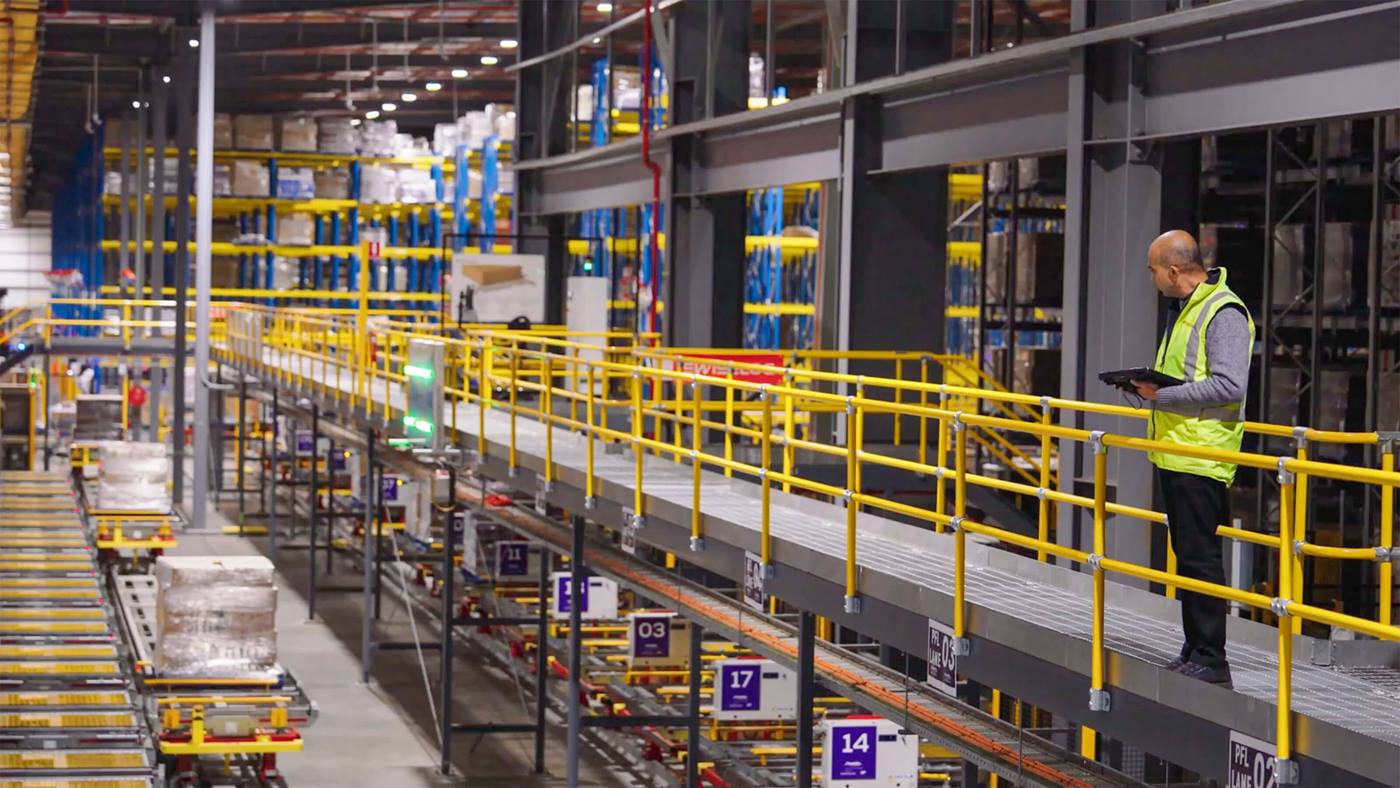
Mondelēz needed to simplify a complex distribution network handling a broad range of confectionery products, while accommodating seasonal peaks and changing consumer demand. Operating across four Victorian distribution centers and off-site storage created additional handling requirements and constrained efficiency.
The company sought to consolidate these operations into one national distribution center, increasing storage capacity, improving productivity, and providing flexibility for future growth without compromising service levels.
The solution - warehouse automation at national scale
Swisslog delivered a warehouse automation solution at Mondelēz’s 47,000 m² national distribution center in Truganina, Victoria, as part of a major $130 million warehouse investment.
The facility consolidates four Victorian distribution centers into one automated hub, supporting the national distribution of chocolate and confectionery brands including Cadbury, The Natural Confectionery Company, Pascall, OB Finest, and Olina’s.
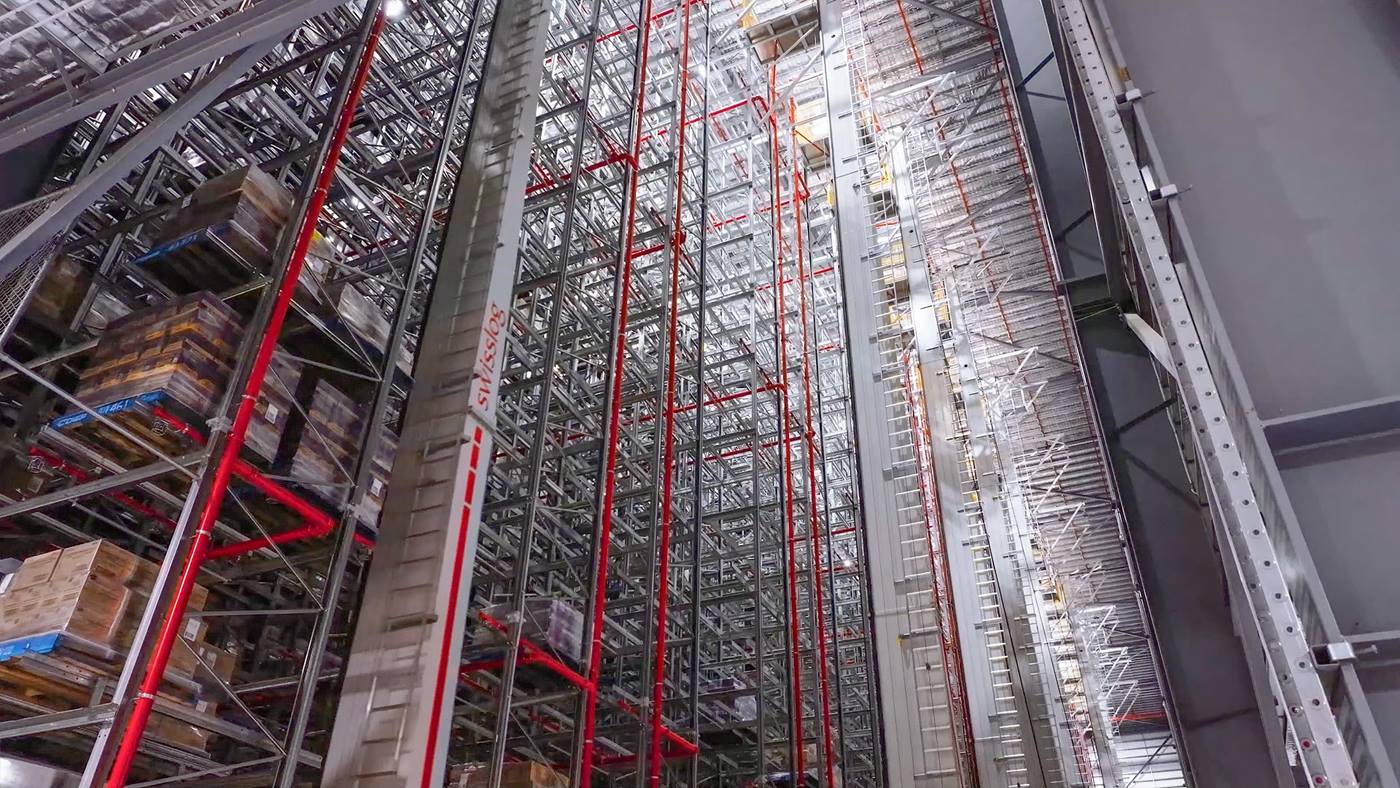
The automated storage and retrieval system (ASRS) serves 56,100 of the facility’s 85,000 total pallet locations, with the facility designed to expand to 96,000 locations. Swisslog’s solution combines high-density storage, automated pallet handling, and SynQ software to synchronize automated and manual operations, improve material flow, and support future demand.
High-density storage and automated pallet handling
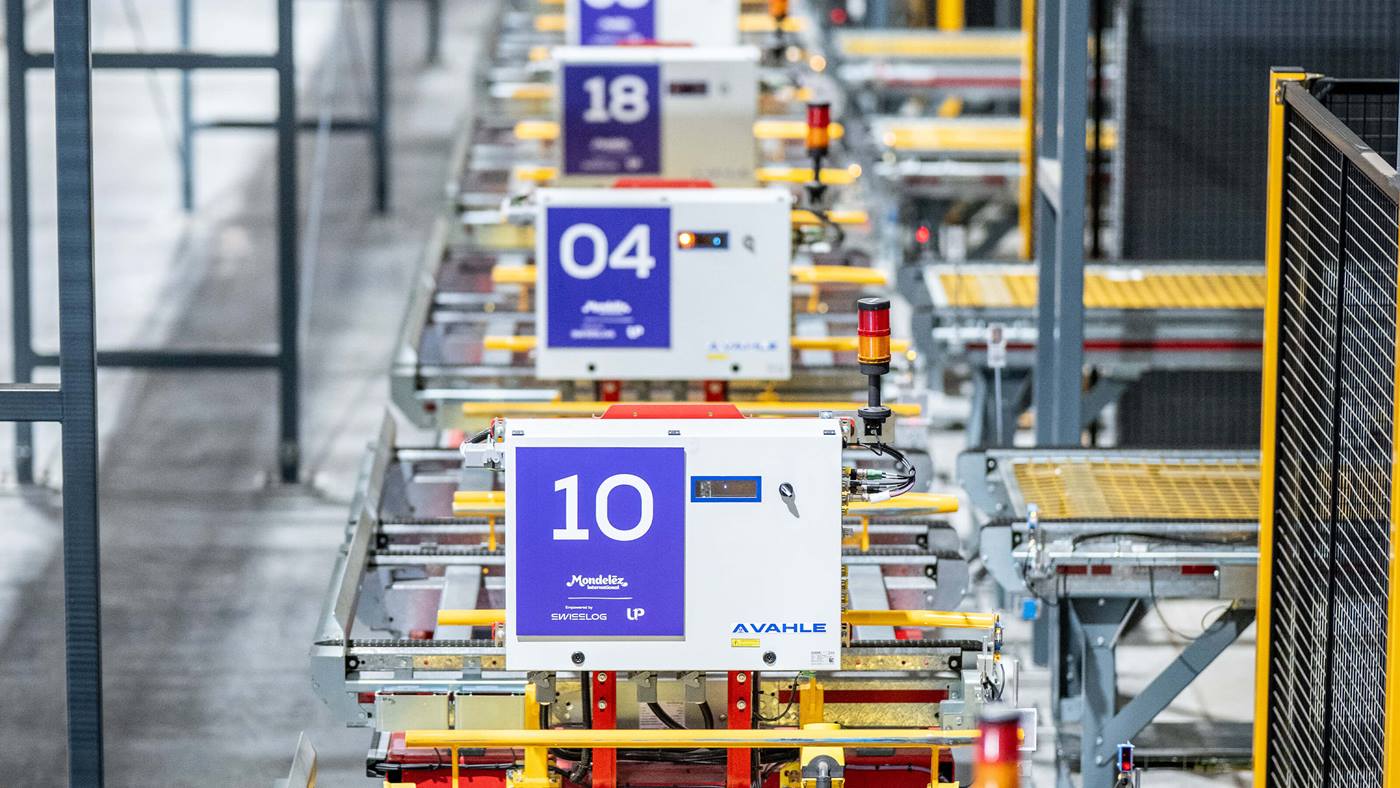
The system features 11 Vectura vertical pallet stacker cranes, each 32 metres tall, with double-deep load handling forks. An inverted monorail circuit with 22 dual-pallet trolleys connects with 490 metres of pallet conveyor, while 16 dual pallet flow lanes stage outbound goods.
The system is designed to process 218 inbound pallets and 255 outbound pallets per hour. Its additional throughput capability across cranes, monorails, and conveyors provides operational redundancy, while double-deep racking maximizes storage density and selectivity.
Intelligent warehouse software
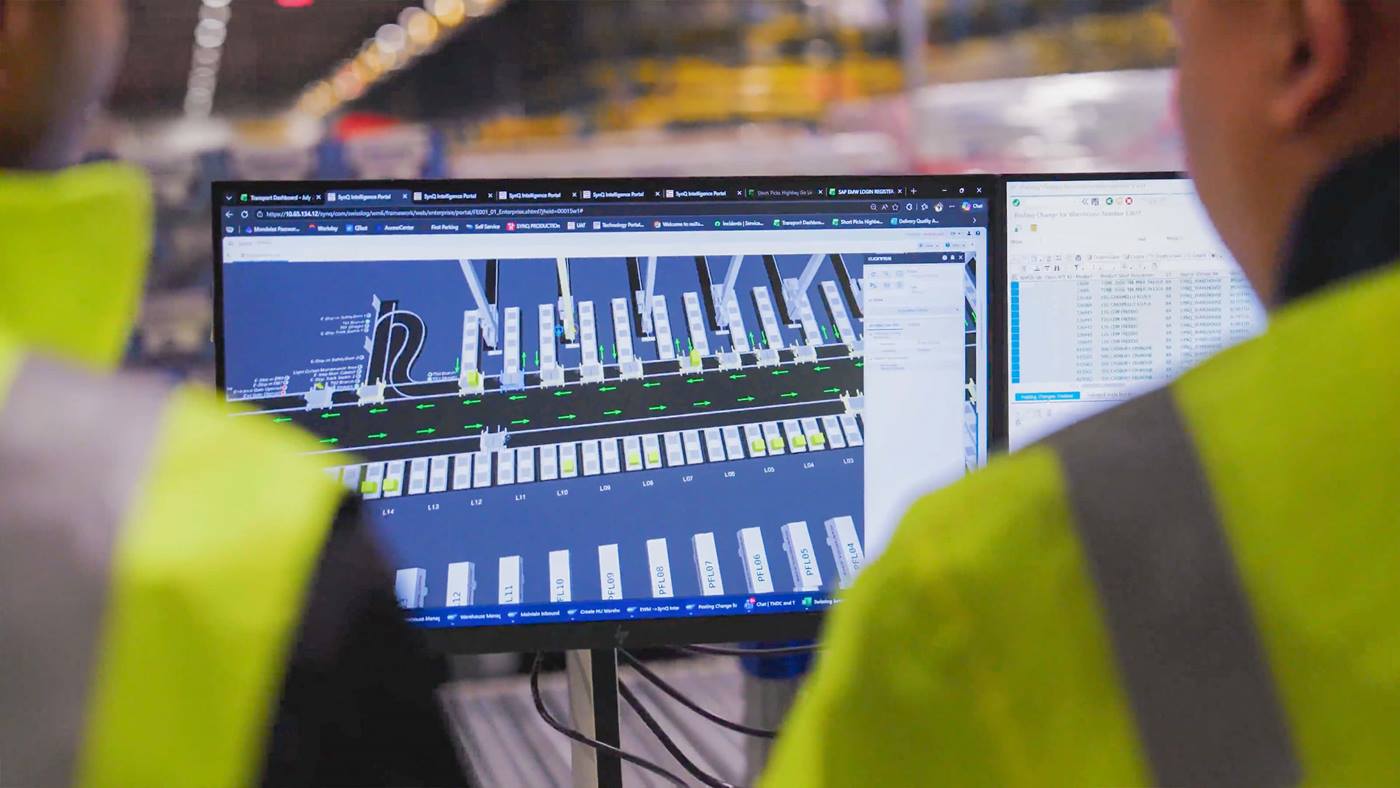
Swisslog’s SynQ software coordinates automated and manual warehouse operations, synchronizing equipment performance and providing operational visibility through business intelligence tools.
The platform supports real-time monitoring and informed decision-making, helping operators manage inventory flows, respond to changing demand, and maintain efficient warehouse operations.
The result - a smarter, more connected warehouse operation
By consolidating four Victorian distribution centers into one national hub, Mondelēz eliminates double handling and removes more than 104,000 pallet movements annually, equivalent to approximately 191,000 kilometres of travel.
The system has delivered more than 98 per cent availability since go-live, according to the same source. With 86,000 pallet locations and provision to expand to 96,000, the facility provides additional capacity and flexibility for future growth. The system’s designed outbound throughput of 255 pallets per hour supports the efficient movement of confectionery through the national distribution network.
Additionally, Swisslog’s SynQ Independent Business Intelligence tools suite adds value by enabling warehouse operations to work smarter, not harder.
SynQ looks after both the automated and manual operations for Mondelēz, and it is a significant win that such a major household name chose Swisslog for the excellent value and return on investment of their warehouse automation.
Safety and sustainability
The automated solution improves operational safety, reduces handling errors, supports workforce upskilling, and improves truck turnaround times. The facility also supports Mondelēz’s sustainability ambitions through 100 per cent renewable electricity and approximately 1 MW of solar generation, expected to cover 30 per cent of estimated electricity demand.
The consolidation of distribution operations also eliminates unnecessary pallet movements and associated transport kilometres, supporting more efficient supply chain operations.
Key project details
| Facility | 47,000 m² national distribution center |
|---|---|
| Project investment | Part of a $130 million warehouse upgrade |
| Network consolidation | Four Victorian distribution centers into one national hub |
| Total facility pallet locations | 85,000 |
| Automated high-bay pallet locations | 56,100 |
| Future facility capacity | Up to 96,000 pallet locations |
| Storage capacity increase | 60% |
| ASRS cranes | 11 Vectura vertical stacker cranes, each 32 metres tall |
| Racking | Double-deep |
| Monorail | 22 dual-pallet trolleys |
| Conveyors | 490 metres |
| Dispatch staging | 16 dual pallet flow lanes |
| Designed inbound throughput | 218 pallets per hour |
| Designed outbound throughput | 255 pallets per hour |
| Reported system availability | More than 98% since go-live |
| Annual reduction in pallet movements | More than 104,000 |
| Equivalent travel eliminated | Approximately 191,000 kilometres annually |
| Software | Swisslog SynQ |
| Energy | 100% renewable electricity and approximately 1 MW of solar generation |
| Solar contribution | Approximately 30% of estimated facility electricity demand |
| Green building target | 5 Green Star Design Rating, Green Building Council of Australia |